Define what the buffer must do
Specify a zero-pressure accumulation conveyor by the behaviour you need when the next machine stops. The buying question is not simply whether the conveyor can move cartons. It is how it will hold, release and transfer your actual loads without relying on a growing queue of cartons pressing together. Hytrol describes this conveyor category as spaced accumulation controlled in zones. That describes a handling approach, not a guaranteed result for every package and operating sequence.
Write down why the buffer is needed. Does it absorb short interruptions at packing, wait for a merge, or present cartons individually to a downstream process? Give the supplier the expected interruption pattern and the available conveyor footprint. Ask for a proposed usable storage arrangement and a release sequence. Keep storage requirements distinct from sustained line throughput so a quotation does not answer one question while leaving the other undefined.
Document the carton envelope
Provide the smallest and largest carton dimensions, weight range, travel orientation and the condition of the surface resting on the rollers. Include representative examples of the packages you actually handle, rather than only a nominal case size. Ask the supplier to identify packages that need a different handling arrangement and to explain how those exceptions will be managed. A trial using an easy carton is not a complete acceptance test for a mixed-case operation.
Interroll's ConveyorControl manual describes an arrangement with one load in each zone, held until the downstream zone is available. Ask the proposed supplier how its own zone arrangement handles your longest cartons and mixtures of sizes. Request a drawing that shows the intended stopping positions and transitions. Do not convert a general description of zones into an assumed zone length or a package-capacity guarantee; those details belong to the actual design and product mix.
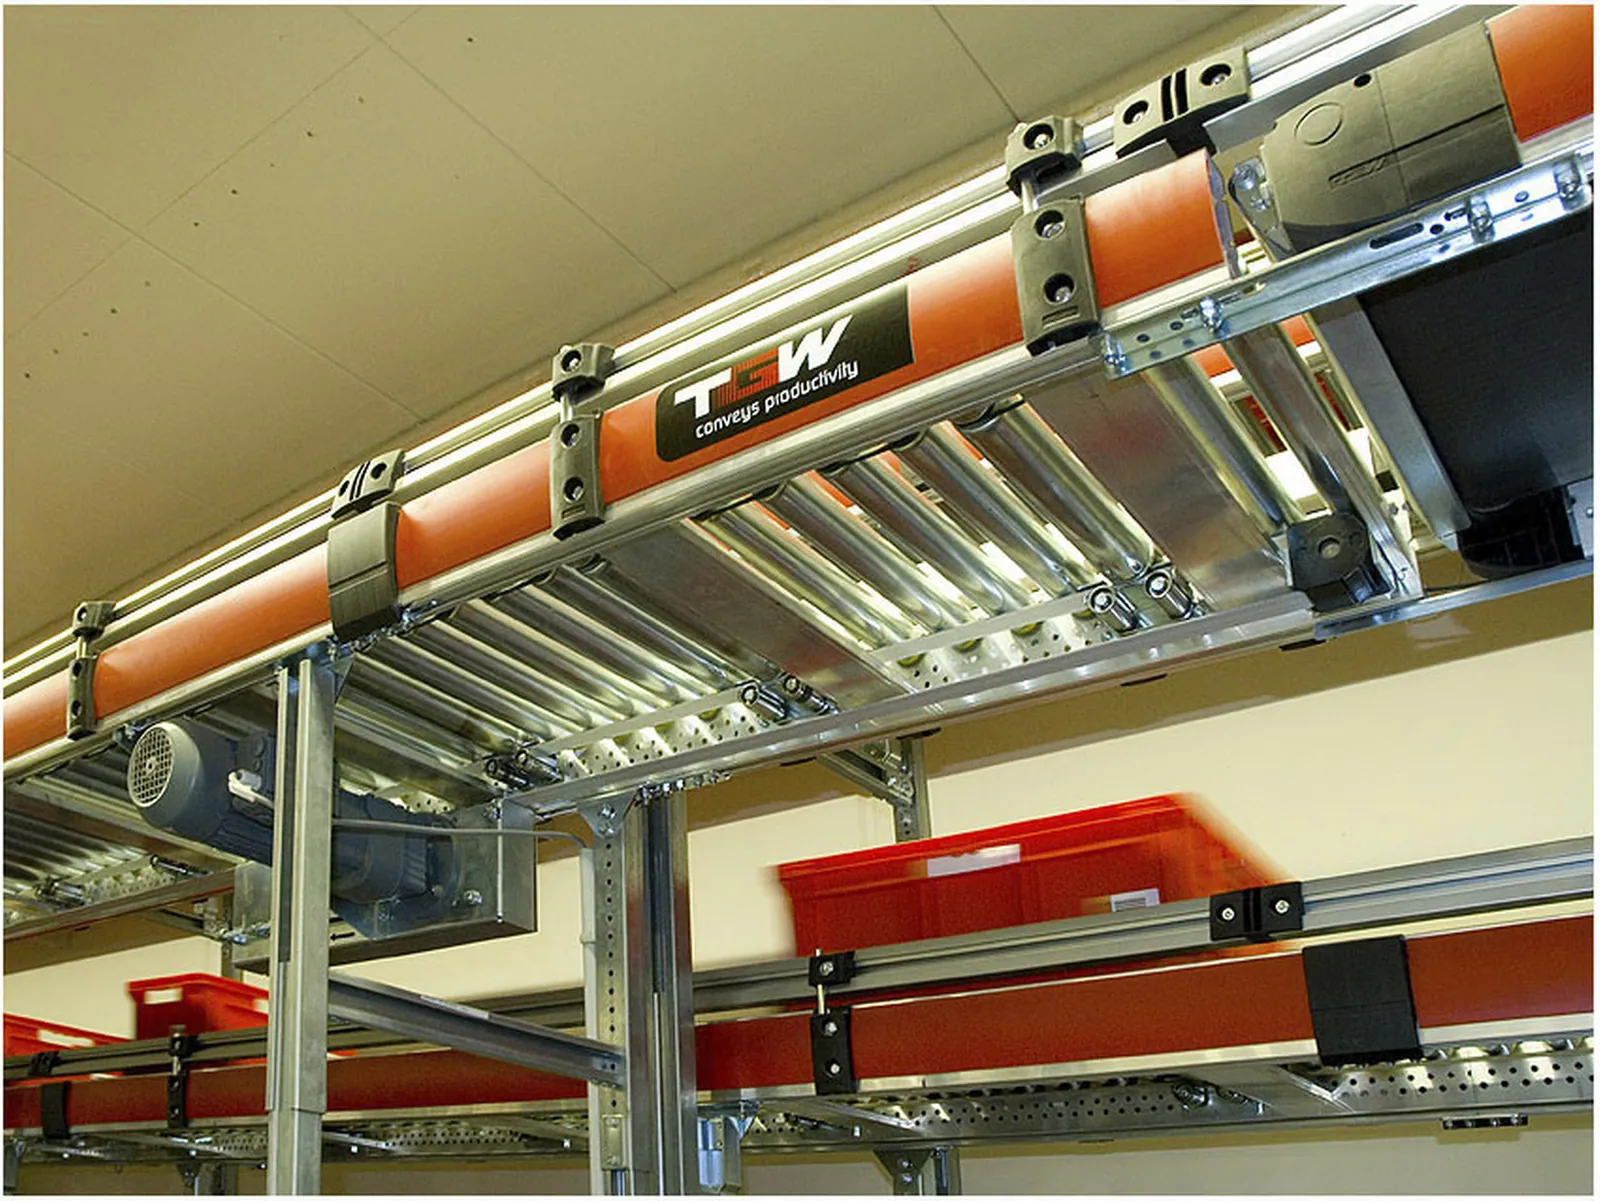
Specify release and interfaces
Describe the sequence at the discharge in plain language. Should cartons leave individually, in groups, or according to a downstream request? What should the conveyor do when the destination becomes unavailable? Hytrol's carton-singulation guidance discusses release-mode selection as part of controlling carton flow. Use that as a reason to ask for the actual sequence, rather than accepting an operating-mode name as a complete specification.
Interroll's ZoneControl product information identifies communication between neighbouring zones and describes that controller's interface scope. A similar-looking controller need not offer the same interfaces. Ask the integrator to document who supplies the controls, what signals cross the equipment boundary and which machine owns the permission to release a carton. Request a sequence description for startup, normal accumulation, planned stopping and fault recovery. Resolve these responsibilities before ordering separate mechanical and controls packages.
Test the awkward conditions
Create an acceptance trial that includes the difficult combinations in your product list. Ask for mixed sizes, the lightest and heaviest representative cartons, and arrivals close together where that occurs in production. Agree how the trial will check stopping positions, spacing and transfer into the next machine. Record any package exclusions and the conditions behind the supplier's stated throughput, rather than treating conveyor speed alone as proof of line performance.
Also agree how unavailable downstream equipment and a simulated fault will be tested safely. Ask what the operator sees, which upstream sections stop and how an authorised restart is initiated. Define how to identify an unsuccessful trial and what correction or retest follows. These are proposed buying checks, not instructions to create a live jam or reach between moving cartons. All testing must follow the responsible team's approved procedure and maintain the required guarding and safe access.
Buy a maintainable system
Ask for the final zone layout, controls drawings, parameter record, replacement-component list and troubleshooting instructions. Identify which adjustments the site's staff may make and which require supplier support. Request an explanation of how a replacement sensor, drive or controller is selected and checked. An order that includes the conveyor but leaves those documents optional can make an otherwise straightforward future repair harder to manage.
Compare suppliers against the same carton envelope and acceptance sequence. Clarify exclusions for upstream equipment, downstream transfers, electrical installation, commissioning and staff training. Where a bidder claims lower energy use or reduced damage, ask for the comparison basis and how the claim would be checked for your duty. Choose on the demonstrated handling and documented integration scope, rather than assuming that the words zero pressure resolve every operating and maintenance question.
This guide helps define questions and requirements. Technical decisions require application documentation and review.
Sources
Hytrol: Zero-Pressure Accumulation Conveyor ↗Explains spaced, zone-based accumulation. It does not specify a conveyor for the reader's carton mix.
Interroll: ZoneControl ↗Documents one controller's adjacent-zone communication and interface scope, not universal controller compatibility.
Interroll: ConveyorControl Operating Manual ↗The function description explains single-load zones and downstream availability. It concerns the documented system.
Hytrol: How to Maintain Carton Singulation ↗Discusses carton flow and release-mode choices. No universal speed or throughput figure is adopted here.